By Jack Sun · Updated October 20, 2026
Quick definition: Metal fibers are slender fibers made from metals or alloys. Production routes include bundle drawing, mechanical cutting and melt-based processes. To make sintered felt, the fibers then undergo web formation, layup and sintering to create a connected porous structure. Fiber production and felt manufacturing are related but distinct stages. [1][2]
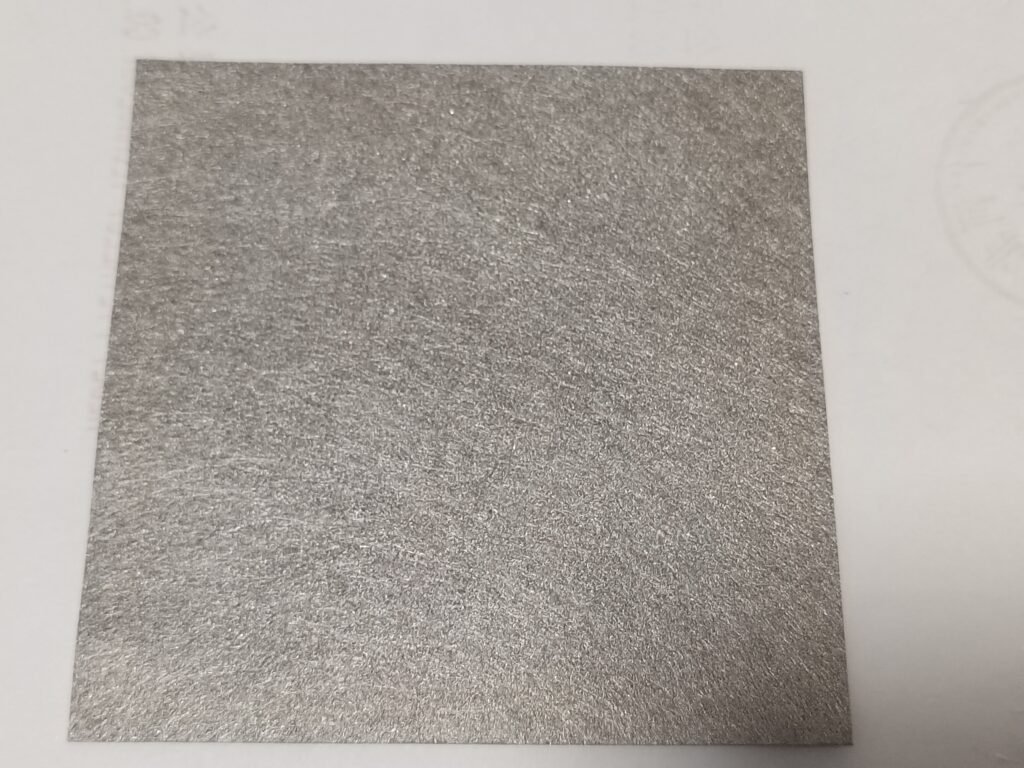
A sheet of sintered metal fiber felt resembles a fine metallic fleece. Its surface contains interlaced fibers and spaces between them. Where do those fibers come from? Is making felt simply a matter of cutting ordinary wire into short lengths?
Cutting to length can be one operation, but fiber preparation also involves size, shape, composition and surface condition. Understanding these features helps explain why sheets with the same material designation and similar thickness can still differ.
This article concerns metal and alloy fibers used in sintered metal felt.
Common metal fiber manufacturing methods
Metal can become fiber through solid-state drawing or cutting, or through a process starting from molten metal. Each route has material and equipment requirements. One process is not suitable for every metal.
Bundle drawing
In bundle drawing, multiple wires are combined within a covering or matrix to form a composite bundle. Drawing reduces the dimensions. The covering or matrix is subsequently removed to release the fibers. Bekaert describes this sequence in its manufacturing information. [1]
The simple picture is that many wires become finer together before separation. Separation and cleaning belong in the explanation: the drawn composite bundle is not yet the same as clean, separated fiber ready for subsequent processing.
The matrix, its removal and the residues requiring control depend on the actual route and material. A general description should not become a universal chemical recipe.
Mechanical cutting and foil shaving
Machining produces slender fibers by cutting material from a metal workpiece. Foil shaving uses metal foil as its starting material. Both involve cutting, but the starting form and detailed processes differ.
Purpose-made cut fibers should not be confused with arbitrary machining swarf. Fiber production requires control of shape and dimensions. Different methods can produce different cross-sections and size distributions. Manufacturer information and patents describe these distinctions. [2][3]
Consequently, the useful question is what a particular batch contains. The label “machined fiber” alone neither establishes poor quality nor demonstrates suitability for every fine-felt application.
Melt-based fiber production
Other routes extract or form fibers from molten metal, which then solidifies during cooling. Specific melt-based techniques should be identified rather than treated as interchangeable.
The material, equipment and process constrain the available shape and size range. [3] The production name provides background; actual fiber characteristics and finished-product verification establish suitability. Omitting drawing does not by itself prove a lower cost or a better result.
Where metal fibers can differ
The manufacturing route affects fiber characteristics, but does not alone determine felt quality.
Diameter and equivalent diameter
Metal fibers are not necessarily circular in cross-section. For a noncircular fiber, a document may use equivalent diameter: the diameter of a circle with the same cross-sectional area. [3]
Two fibers with the same stated dimension may therefore have different shapes. Confirming the dimensional definition and measurement method helps avoid comparing unlike quantities.
Average size and size distribution
An average describes an overall level, not the dimensions of every fiber. Two batches can have similar averages but different proportions of relatively fine and coarse fibers.
A narrower distribution is not automatically better for every purpose. Deliberately combining sizes to form a designed structure differs from an uncontrolled change in the raw material.
Length, shape and dispersion
Fibers must disperse and form an interconnected layer. Length, curvature and agglomeration therefore provide useful clues when interpreting web formation.
An engineering implication is to observe subsequent web formation when the raw material changes. Looking only at the alloy designation can leave a source of local unevenness unexplained while later processing is repeatedly adjusted.
Composition and surface condition
The grade describes composition; surface condition addresses what is present at the fiber surface. Where a route uses a matrix, covering or processing aid, the relevant removal and cleanliness requirements should follow that process.
Research on bundle-drawn stainless steel fibers also considers the influence of matrix elements at the fiber surface. [4] This supports distinguishing composition from surface condition, without treating every oxide or residue as the same problem.
From metal fibers to sintered felt
A general sequence is fiber preparation, web formation and layup, sintering, then the finishing and inspection required for the product. The detailed order and equipment vary.
Forming the porous structure
The fibers form layers that are combined to the intended construction. Distribution across the sheet and through its thickness matters. Single layers, multiple layers and combinations of fiber sizes are structural choices; “denser is better” is not a general rule.
Consider distribution, mass per unit area and thickness together. Total sheet weight alone can conceal local variation.
Bonding at fiber contacts
Sintering creates metallurgical bonds at fiber contacts, producing a porous network with mechanical integrity. Manufacturer literature describes intermetallic diffusion bonding in such structures. [2]
Temperature, time and atmosphere must suit the material and construction. One universal cycle cannot cover all metal felts. Increasing temperature without examining bonds, dimensional changes and product requirements may leave the original issue unresolved.
Finishing and inspection
Depending on the part, subsequent work can include leveling, calendering, cutting or forming. Acceptance should follow the drawing and agreed requirements.
Fiber information helps explain a product but cannot replace finished-product checks. Equally, passing a thickness check does not establish every other characteristic. Fiber diameter, pore structure and filtration rating are different quantities and cannot be directly substituted for one another.
For the later stages, see how layup and sintering shape metal fiber felt.
Understanding and investigating differences
For an existing drawing, manufacturing communication normally starts with that drawing. Questions should address the specific details affecting fabrication or acceptance.
Describe the observed difference first
An apparent difference can concern fiber size, length, cross-section, dispersion or observation conditions. Turn “it looks different” into a describable or measurable observation before checking batch and process information.
Assuming that a color difference proves the wrong alloy, or that finer-looking fibers prove better quality, can send the investigation in the wrong direction.
Equal thickness does not describe the whole structure
Thickness cannot alone describe fiber distribution, pore connectivity or bonding. Where a test or service result differs, examine the characteristics relevant to that issue.
This is not a reason to add every possible test to every order. The purpose is to connect the check to the actual question.
Trace local abnormalities through the process
Start with the location, extent and nature of an abnormality, then review raw material, layup, sintering and finishing as relevant. Local thickness variation and an entire sheet being too thick can require different investigations.
These are diagnostic directions, not causes established from appearance alone. Repeatedly changing one parameter without confirmation can alter the symptom while leaving the cause unresolved.
Frequently asked questions
How do metal fibers differ from ordinary wire?
Size ranges can overlap. In this context, “fiber” also describes the form and use of the material as feedstock for a web. A single universal diameter boundary does not distinguish every metal fiber from wire.
Are bundle-drawn fibers always better than machined fibers?
No. Evaluate material, dimensions, shape, consistency and the resulting felt. The route alone does not rank all products.
Do finer fibers always mean better filtration?
No. Finished structure, thickness, pore connectivity, operating conditions and the test method also matter. Fiber diameter is not a filtration rating.
Must a buyer specify the fiber production method?
Not for every order. An existing drawing and agreed acceptance requirements can provide the starting point. A specified process restriction or a particular performance problem may require more detailed discussion.
Are fiber producers and felt manufacturers necessarily the same company?
No. One company can perform both stages, or upstream fiber production and downstream felt manufacturing can be separate. Descriptions of manufacturing capability should reflect the actual operations.
Conclusion
Fiber production establishes important material, dimensional and surface characteristics. Layup, sintering and finishing then shape the finished porous product.
Connecting these stages makes differences easier to understand and investigate. For drawing-based work, the practical focus remains understanding the drawing, meeting agreed requirements and addressing significant uncertainties directly.
See our sintered metal fiber felt products for related supply forms.
Technical references
- Bekaert — Metal fiber production and products.
- Bekaert — An introduction to Metal Fiber Technology.
- US20150176112A1 — Mass of metal fibers and process for making such a mass.
- US7166174B2 — Bundle drawn stainless steel fibers.
The sources support process principles. Patent-specific examples and manufacturer performance claims are not universal specifications or evidence of our own equipment.
By Jack Sun. Jack Sun has long worked in metal wire mesh weaving and industrial filter-element manufacturing. Our company is based in Anping, Hengshui, Hebei, China.